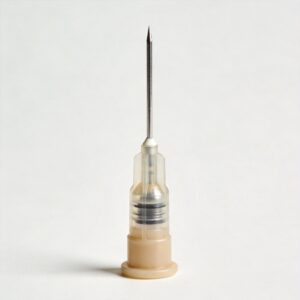
ISO 9626 is the international standard that defines the material, dimensions, and mechanical performance requirements for stainless steel needle tubing used in medical needles. It specifies designated metric sizes (from 0.18 mm to 3.4 mm outer diameter), four wall-thickness types (regular, thin, extra-thin, ultra-thin), chemical composition for austenitic stainless steel, and tolerances for outer diameter, inner diameter, and concentricity. If you are specifying, sourcing, or inspecting needle tubing, this standard is the reference document you measure against. After reading this guide, you will be able to read an ISO 9626 size table, verify a tubing lot against its dimensional tolerances, and identify the three most common compliance failures before they reach your production line.
Table of Contents
What ISO 9626 Actually Covers
ISO 9626 (currently published as ISO 9626:2016, “Stainless steel needle tubing for the manufacture of medical devices”) is maintained by ISO Technical Committee 84, which handles transfusion, infusion, and injection equipment. The standard exists because a “21G needle” is not a legally meaningful specification on its own — two suppliers can both claim 21G and deliver tubing that differs by 0.05 mm in inner diameter, which changes flow rate and patient pain perception.
Material requirements
The standard restricts tubing to austenitic stainless steel in the 300 series, most commonly grades 304 and 316L. It sets limits on carbon, chromium, nickel, and molybdenum content, and requires the tubing to be corrosion-resistant under the test conditions defined in the standard. A key point: ISO 9626 covers tubing, not the finished needle assembly. Cannula grinding, lubrication, and hub bonding fall under separate standards such as ISO 7864 for hypodermic needles.
Dimension requirements
Each designated size has a nominal outer diameter (OD) and a permitted tolerance. Wall thickness is classified into four types, and for each combination of size and wall type, the standard defines a nominal inner diameter (ID) and its tolerance. The table below shows representative entries — always confirm against the full published table before writing a purchase specification.
| Designated size | Nominal OD (mm) | Wall type | Nominal ID (mm) |
|---|---|---|---|
| 18G | 1.20 | Regular | 0.86 |
| 21G | 0.80 | Regular | 0.51 |
| 21G | 0.80 | Thin | 0.56 |
| 25G | 0.50 | Regular | 0.26 |
| 30G | 0.30 | Extra-thin | 0.16 |
| 33G | 0.20 | Ultra-thin | 0.11 |
Note the pattern: as wall type moves from regular toward ultra-thin, the ID grows while the OD stays fixed. This is the single most useful fact in the standard for designers — you can increase flow rate without increasing needle gauge simply by specifying a thinner wall.
Mechanical and surface requirements
The standard also addresses stiffness (via a bend test), resistance to breakage, and internal surface cleanliness. The bend test is a cantilever deflection test: a defined length of tubing is fixed at one end and loaded at the other, and the deflection must fall within a specified range for that size. Tubing that is too stiff risks patient injury during a bend; tubing that is too soft risks buckling during insertion.
How to Verify Tubing Against ISO 9626
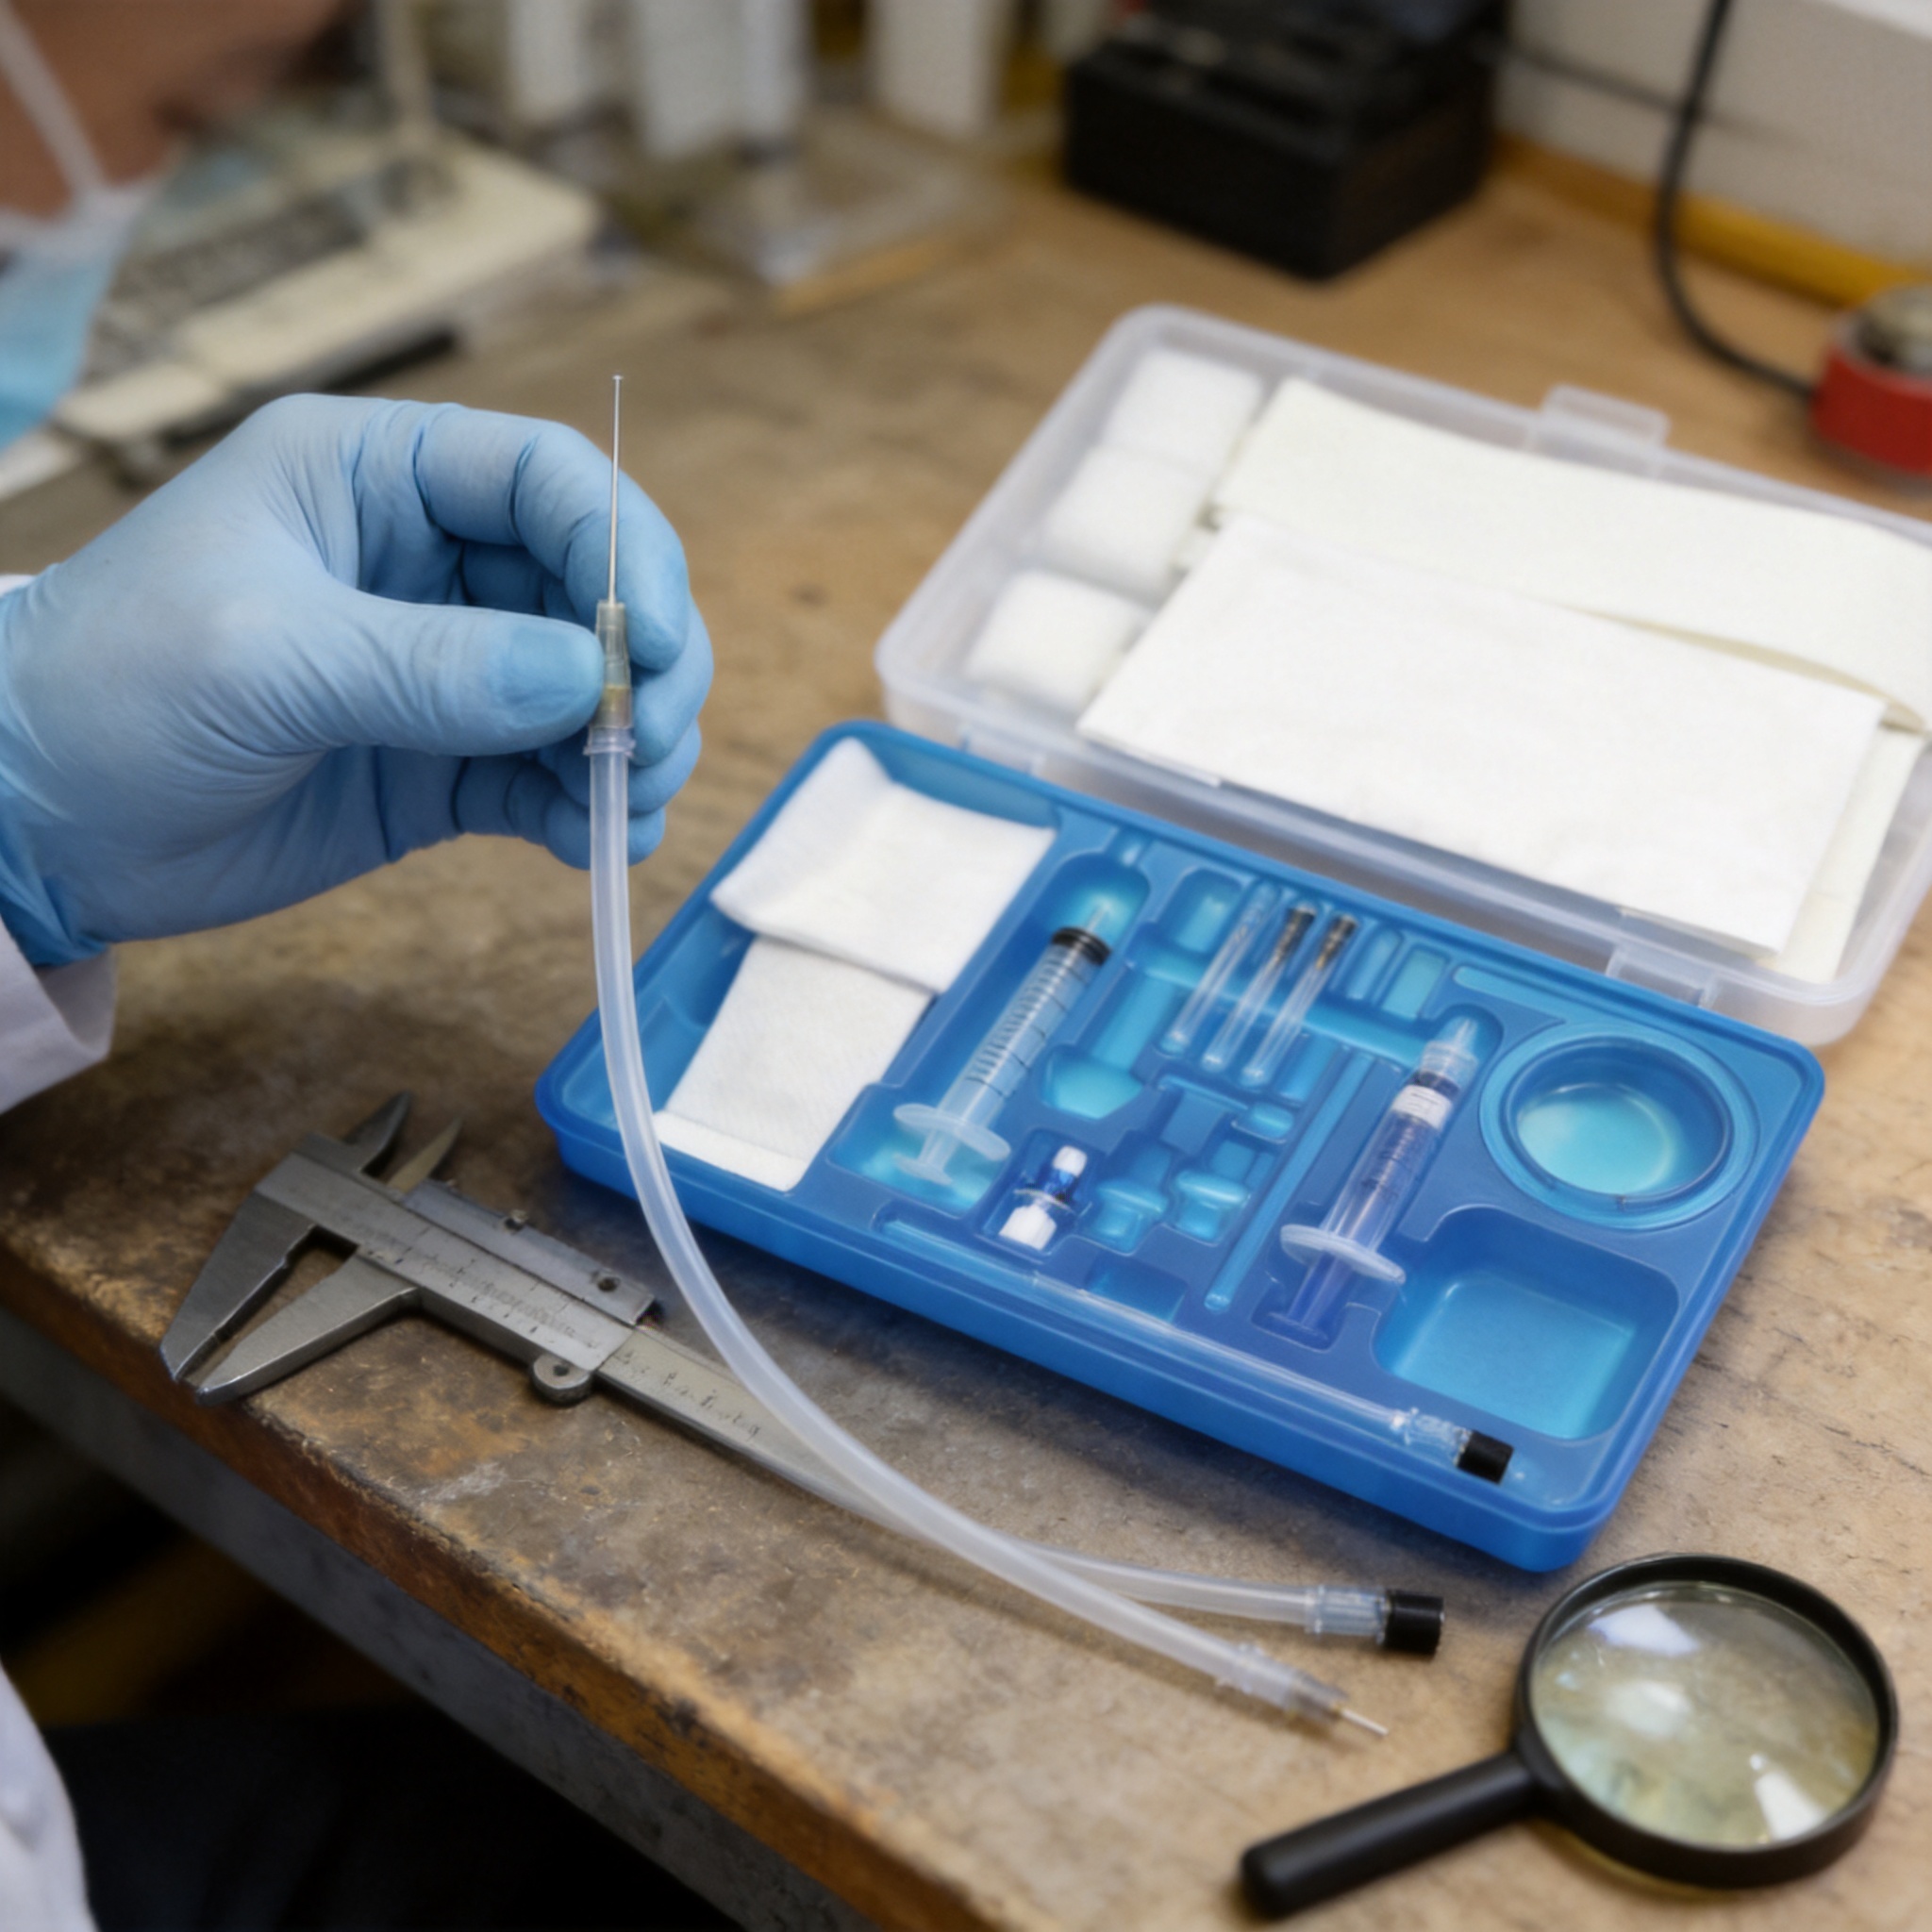
You can run a compliance check on an incoming tubing lot in about two hours with basic metrology equipment. Follow these steps in order.
- Confirm the supplier’s declared designation. Ask for the size (e.g., 23G), wall type (e.g., thin), and steel grade (e.g., 304). If any of the three is missing, stop — you cannot verify against ISO 9626 without all three.
- Pull the correct nominal values from the ISO 9626 table. Record nominal OD, OD tolerance, nominal ID, and ID tolerance for that size/wall combination.
- Condition the samples. Let tubing sit at 20 ± 5 °C for at least 30 minutes. Stainless steel expands roughly 16 µm per meter per °C, so a cold lot measured immediately after winter shipping will read undersized.
- Measure OD at five points. Use a calibrated micrometer with flat anvils, taking readings at 0°, 45°, 90°, 135°, and 180° around the circumference at a single cross-section. Record all five.
- Measure ID by pin gauge or optical method. Pin gauges are fastest: a “go” pin at nominal ID minus tolerance and a “no-go” pin at nominal ID plus tolerance. For thin walls, use optical comparators instead — pin gauges can deform the tube.
- Calculate concentricity. Subtract the minimum wall thickness from the maximum wall thickness at the same cross-section. Compare against the standard’s limit for that size.
- Run the bend test. Clamp a 50 mm length, apply the specified load for that size, and measure deflection. Compare to the range in the standard.
- Document and disposition. Mark the lot pass or fail per characteristic, not as a whole. A lot can pass OD and fail ID, and that distinction matters for your supplier conversation.
For reference on how these tubing dimensions feed into finished-device requirements, the U.S. FDA’s guidance library at fda.gov/medical-devices is the authoritative starting point for device classification questions.
Common Mistakes and How to Fix Them
These three failures account for the majority of ISO 9626 disputes I have seen in 15 years of supplier qualification work.
Mistake 1: Treating gauge number as a complete specification
Symptom: You order “25G tubing” from two suppliers and the finished needles deliver noticeably different flow rates. Fix: Always specify size plus wall type. A 25G regular-wall tube has a nominal ID of 0.26 mm; a 25G thin-wall tube is larger. The gauge number alone pins only the OD.
Mistake 2: Measuring only one cross-section
Symptom: Incoming inspection passes, but 3–5% of finished needles fail flow testing. Fix: Draw tubing from both ends and the middle of the coil. OD drift along a 3,000 mm coil is common after drawing, and a single mid-coil measurement hides it. Measure at least three positions per sample.
Mistake 3: Using the wrong instrument for thin walls
Symptom: ID readings are inconsistent between operators, varying by more than the tolerance band. Fix: Contact pin gauges apply radial force that can ovalize extra-thin and ultra-thin walls. Switch to a non-contact optical comparator or air gauge for any wall type below “thin,” and re-qualify your measurement system with a gauge R&R study.
Mistake 4: Ignoring the bend test until clinical use
Symptom: Needles bend or break during procedures despite passing dimensional checks. Fix: Add the cantilever bend test to your incoming inspection for any new supplier, then reduce to periodic sampling once three consecutive lots pass.
FAQ
Is ISO 9626 the same as ISO 7864? No. ISO 9626 covers the raw stainless steel tubing. ISO 7864 covers finished sterile hypodermic needles for single use, including the cannula, hub, and cap. You need both if you manufacture finished needles.
Does ISO 9626 apply to non-stainless materials? No. The standard is written specifically for austenitic stainless steel. If you are evaluating nitinol, titanium, or polymer cannulas, ISO 9626 does not apply and you need a different specification framework.
What is the smallest size in ISO 9626? The standard’s designated size range extends down to approximately 0.18 mm OD, which corresponds to sizes used in ophthalmic and fine-dosing applications. Sizes below that are typically custom and outside the standard’s scope.
How often should I re-verify a supplier? A practical rule: full dimensional verification on every new supplier and every new lot for the first three lots, then reduce to one lot per quarter if three consecutive lots pass all characteristics. Any supplier process change resets the clock to full verification.
Can a supplier claim ISO 9626 compliance without a certificate? A declaration alone is not evidence. Request the actual dimensional test report with measured values, the steel grade certificate (EN 10204 3.1 is standard for this), and the bend test data. If they cannot produce measured values, treat the claim as unverified.
For the official standard text and current edition status, check the ISO catalogue entry at iso.org. For material certification conventions, the EN 10204 framework referenced above is published by the European Committee for Standardization.
Disclosure: This article is based on hands-on supplier qualification and incoming inspection work. No supplier, brand, or product is endorsed, and no compensation was received for this content.


 English
 Deutsch
 Français
 Русский
 Español
 Português